Quarry Turnkey Drilling Projects: Hole Pattern Design, Equipment List, and How to Measure Whether It Actually Works
"Turnkey" means the buyer turns a key and the operation runs. In practice it means whatever the supplier's scope of supply says it means, and those scopes vary enormously between quotations that look comparable on price. This article covers how to size a quarry drilling package from the production target backwards, what belongs on the equipment list, and the benchmarks that tell you within the first month whether the package was specified correctly.
Three Turnkey Quotes, One Missing Compressor
An aggregate producer in West Africa was scoping a new bench and asked three suppliers for a turnkey quarry drilling package. The lowest quote came in 22 percent below the other two. He took it.
The rig arrived. It was a crawler DTH unit that requires an external air supply — a perfectly good machine, but not an integrated one. There was no compressor in the scope of supply. Reading the quotation again after delivery, he found it had never said there was.
The second problem surfaced at the same time. He was drilling Ø115 mm blast holes. The tooling package in the quote was built around a Ø90 mm hammer and matching bits. The hammer physically could not produce the hole he needed.
The rig sat in the yard for eleven days waiting on a compressor to be sourced and shipped. By the time the first hole was drilled, the 22 percent saving had been consumed several times over in delay, urgent freight, and a tooling package that had to be re-bought.
Nothing in that quotation was dishonest. The scope of supply was written accurately. It was simply narrower than the buyer assumed, and "turnkey" on the cover page did nothing to change that.
Work Backwards From the Production Target, Not Forwards From the Rig
Most package scoping starts with a rig model and works outward. That sequence produces equipment that is internally consistent but not necessarily matched to what the quarry has to produce.
The correct order runs the other way, and each step constrains the next.
Start with tonnage required. What does the crusher need per day, and how many days per month does the operation run? This is the only number the business actually cares about.
Convert tonnage to blasted volume. Divide by the in-situ density of the rock to get cubic metres that must be blasted per period.
Convert volume to drilled metres. This is where pattern design enters. Each blast hole breaks a volume defined by burden × spacing × bench height. Divide required volume by volume-per-hole to get hole count, then multiply by hole depth including subdrill to get metres.
Convert drilled metres to rig hours. Apply a realistic penetration rate for the formation, then apply a utilisation factor — the fraction of shift time the rig is actually drilling rather than tramming, setting up, waiting, or under maintenance.
Then select the rig. Now you know the hole diameter, hole depth, and daily metre requirement the machine has to satisfy.
The step that gets skipped is utilisation. A rig that penetrates at 30 m/h does not drill 240 metres in an eight-hour shift. Tramming between holes, collaring, rod handling, refuelling, and operator breaks consume a substantial share of the shift. Our quarry drilling solution uses a shift target of 180–240 metres per 8-hour shift for high-throughput aggregate production, and that figure already contains a realistic utilisation assumption. Scoping against raw penetration rate rather than shift output is the most common way a package ends up undersized.
Hole Pattern Design: What the Package Has to Drill
Pattern design determines the hole count, and hole count determines everything about the equipment package. It is a drilling specification before it is a blasting specification.
Burden — the distance from a hole to the nearest free face — starts at roughly 25 to 35 times hole diameter, lower in hard competent rock and higher in softer or jointed formations. Spacing typically runs 1.1 to 1.3 times burden. Bench height divided by burden gives the stiffness ratio, which should stay at 2 or above to keep blast energy moving forward rather than venting upward as flyrock.
The full derivation, including how to read a muckpile to diagnose a pattern that is not working, is set out in our guide to quarry blast hole pattern design. For package scoping, the relevant output is simpler: how many metres per day, at what diameter, to what depth.
Hole diameter is the decision that propagates furthest. It sets hammer size, which sets air demand, which sets compressor size, which sets fuel consumption and mobilisation weight. It also sets the pattern dimensions, which sets hole count for a given production target.
There is a genuine trade-off here that buyers rarely see stated. Larger holes mean fewer holes for the same volume — less drilling time, less rig wear, fewer detonators. But larger holes also mean a bigger compressor, higher fuel burn, coarser fragmentation, and a pattern that may be too coarse for the crusher's feed size requirement. Smaller holes give better fragmentation control and a lighter equipment package, at the cost of more drilled metres per tonne.
The right answer depends on what the crusher wants and what the site can support. A quarry feeding a jaw crusher with a large gape tolerates coarser fragmentation than one feeding an impactor. That constraint should be established before hole diameter is chosen, not after.
Drilling Method: What the Formation Decides
The method decision follows from rock hardness and hole depth, and it changes the equipment list substantially.
| Criteria |
DTH (Down-The-Hole) |
Top Hammer |
| Rock hardness range |
f = 6–20, all hardness |
f = 6–14, soft to medium only |
| Hole straightness |
±0.5% deviation |
±2–3% deviation |
| Drilling depth |
15–50 m without accuracy loss |
Degrades beyond 15 m |
| Hole diameter range |
50–200 mm |
30–115 mm |
| Energy delivery |
At the bit face, no rod-string loss |
Through the rod string, loss increases with depth |
| Noise |
Lower — hammer works underground |
Higher — impact at surface |
The deviation figures are the ones with financial consequences. At ±0.5 percent, a 20-metre hole ends up within 100 mm of where it was planned. At ±3 percent, the same hole is 600 mm off — which on a 3-metre burden is a 20 percent error at the toe, concentrated at the most confined point in the hole. That is the mechanism that produces toe ridges and oversize, and oversize is what secondary breaking exists to fix.
Top hammer is not the wrong choice — in limestone benches under 15 metres it drills faster and costs less to run. It becomes the wrong choice when depth or hardness pushes it outside its range, and the symptom appears in the muckpile rather than at the rig.
The Equipment List: What a Complete Package Contains
This is the list to check a quotation against, line by line. Anything absent is either the buyer's cost or a delay waiting to happen.
Primary drilling equipment
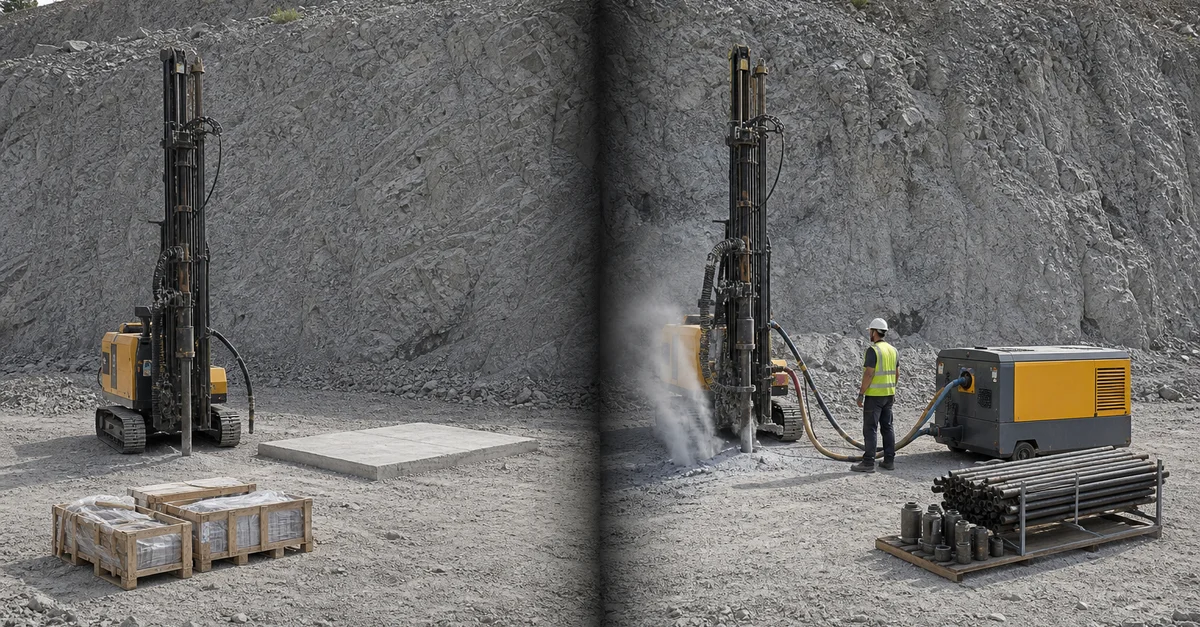
- Drill rig, specified for hole diameter, hole depth, and terrain — including whether the site's bench width and access gradient suit a crawler unit.
- Air supply — and this is the line that must be read carefully. Integrated rigs carry an onboard screw compressor; non-integrated rigs require a separate portable unit. The two produce very different total package costs and very different mobilisation logistics.
Three rig classes cover most quarry applications, and the air supply question resolves differently in each.
| Model class |
Hole diameter |
Max depth |
Power |
Weight |
Air supply |
| HB70 — light duty, electric DTH |
50–80 mm |
15 m |
3 kW motor |
175 kg |
External required |
| KG420T / KG420TH — medium duty crawler |
Ø90–152 mm |
25 m |
58–73.5 kW |
5,050–5,350 kg |
External required |
| KT5H — heavy duty integrated |
90–127 mm |
24 m economic |
162 kW engine |
9,500 kg |
Onboard screw compressor |
The KG420T is a capable rig with a folding mast for fast relocation and four-wheel drive for slopes up to 30 degrees. It also needs a compressor that is not part of the machine. That is not a deficiency — it is a configuration choice with a cost attached, and the cost belongs in the comparison.
Tooling package
- DTH hammer sized to the hole diameter and matched to available air volume and pressure.
- Drill bits — face design and carbide grade selected for the formation, with initial quantity based on expected bit life in that rock rather than a round number.
- Drill rods or pipe — diameter, length, and thread type, in sufficient quantity for maximum hole depth plus spares.
- Adapters, shanks, and subs matched to the rotary head and the hammer thread.
Tooling quantity is where quotations diverge most quietly. One supplier includes a first fill; another includes one bit. Both lines read "DTH bit" on the quotation. How hammer, bit, compressor, and drill pipe have to be selected as one system — and what breaks when they are not — is covered in our guide to aggregate quarry drilling bit and compressor matching.
Support and consumables
- Spare parts package — wear parts sized against formation abrasiveness and project duration, not a generic list.
- Filters and lubricants for the first service intervals of both rig and compressor.
- Dust suppression — dry collection system or water injection, depending on regulation and site conditions.
- Hoses, couplings, and connection hardware between compressor and rig.
Commissioning and support
- Installation and commissioning — remote video-guided, or an engineer on site. These are different costs and different timelines.
- Operator training — including levelling and collaring routine, which is the single largest controllable factor in hole deviation.
- Warranty terms — duration, what is covered, and how a claim is handled from a remote site.
- Technical response commitment — a stated response time in the contract, not an assurance in an email.
A parts package that arrives with the machine is worth more than a faster response time on an order placed after the rig has already stopped. The reasoning behind sizing that package against project duration rather than copying a generic list is set out in our guide to spare parts planning and drilling downtime.
Reading Three Quotations That Are Not Comparable
Turnkey quotations differ in boundary, not just in price. Before comparing totals, establish where each supplier's responsibility stops.
Four questions settle most of it.
Is the air supply inside the scope? If the rig is not integrated and no compressor line item exists, the quotation is for a rig, not a package.
What tooling quantity is included, and at what diameter? Confirm the hammer size matches the hole diameter you actually intend to drill. Confirm the bit quantity against expected bit life in your formation.
Who commissions it, and are they on site? Remote commissioning is legitimate and often sufficient. It is not the same product as an engineer at the bench, and the two should not be compared as if they were.
What does the spare parts package cover, in operating hours? Not item count — hours. A package of twenty parts that covers 200 hours of a 4,000-hour project is a starter kit, not a parts plan.
My view after seeing this pattern repeatedly: the cheapest turnkey quote is usually the one with the narrowest boundary, and the price difference is almost exactly the value of what was left out. That is not a supplier trick. It is what happens when a buyer asks three companies to quote "a turnkey package" without defining the boundary themselves.
The fix sits with the buyer. Issue the equipment list above as the scope, and ask every supplier to price against it, marking any line they exclude. Three quotations against a defined scope are comparable. Three quotations against the word "turnkey" are not.
Efficiency Benchmarks: Proving the Package Was Specified Correctly
A drilling package should be verified against measurable output, and the measurement should start in the first month while the specification is still contestable.
Five benchmarks cover it.
| Benchmark |
What it measures |
What a poor result indicates |
| Metres per shift |
Actual drilled metres per 8-hour shift, all holes |
Undersized rig, insufficient air, or low utilisation from site organisation |
| Rig utilisation |
Percentage of shift time actually drilling |
Excessive tramming, slow rod handling, or unplanned downtime |
| Hole deviation |
Surveyed offset at hole bottom vs planned position |
Setup discipline, feed alignment, or wrong method for the depth |
| Bit life in metres |
Metres drilled per bit before replacement |
Wrong carbide grade, insufficient air for hole cleaning, or over-feeding |
| Secondary breaking rate |
Share of blasted volume needing rework before crushing |
Pattern design, hole deviation, or fragmentation mismatched to crusher |
Secondary breaking deserves particular attention because it is the benchmark that translates drilling quality directly into money. Every oversize boulder requires a hydraulic breaker or a secondary charge before it can be crushed, and that cost sits outside the drilling budget where it is easy to overlook.
Our quarry drilling solution states that maintaining hole deviation below 1.5 percent reduces secondary breaking by up to 40 percent. That figure has a specific implication for how packages should be evaluated: the difference between a rig that holds deviation and one that does not shows up in the secondary breaking line, not in the drilling line. A cheaper rig with looser accuracy can look better on cost per drilled metre while being more expensive per tonne delivered to the crusher.
The related figure from the same source is that misaligned holes and the oversize they produce can cost 10 to 15 percent of daily output value. That is the size of the prize, and it is why deviation is worth measuring rather than assuming.
Cost per metre is the summary number, but it is only meaningful when it includes consumables, fuel, and downtime rather than just the machine. The full breakdown is in our guide to why the real cost of drilling is cost per meter, and the blasting side of the same budget in what a quarry drilling and blasting budget actually contains.
Site Conditions That Change the Package
Four site factors alter equipment selection enough to be worth confirming before a quotation is issued.
Bench width and access gradient. A rig that cannot reach the bench is not a rig. Narrow benches and steep access favour compact or electric units over large crawlers, regardless of what the production target suggests.
Power availability. Grid power at the bench allows electric rigs and electric compressors, which cut running cost substantially. No grid means diesel, which means fuel logistics become part of the operating plan.
Elevation. Compressor output falls with altitude, and the loss is larger than most quotations assume because reduced air density and reduced engine power compound. A package specified at sea-level ratings will underperform on a high site — the correction method is in our guide to high altitude DTH drilling and compressor derating.
Hole geometry beyond vertical. Pre-split holes, inclined production holes, and holes near a crest require mast and boom articulation the rig may not have. A specification sheet lists angles; whether those angles cover your hole schedule is a separate check, set out in our guide to what drill rig mast and boom articulation angles really mean.
Why Welldone Mining
Welldone Mining scopes quarry packages from the production target backwards, and states the boundary of supply explicitly so quotations can be compared against each other rather than against an assumption.
What quarry operators get:
- Package sized from your tonnage requirement. Send your daily production target, formation, bench height, and crusher feed size requirement, and we work back through pattern, hole count, and drilled metres to the rig and compressor that meet it — including the utilisation assumption used, stated openly.
- Air supply resolved inside the quotation. Integrated rig or separate compressor, priced either way, so the comparison is between complete packages rather than between a machine and a package.
- Spare parts sized in operating hours. Wear parts specified against your formation and project duration, quoted with the coverage period stated, so a stopped rig is not the first indication that the parts plan was thin.
Related Solutions
- Quarry Drilling Solution — Rig models, method comparison, and complete drilling packages for hard rock, limestone, and aggregate production.
- Customized Drilling Solution — Restricted access, unusual bench geometry, high altitude, or non-standard hole requirements.
- Quarry Blast Hole Pattern Design — Burden, spacing, stiffness ratio, hole deviation, and reading the muckpile.
- Aggregate Quarry Drilling — Bit and Compressor Matching — Why hammer, bit, compressor, and drill pipe must be selected as one system.
- Quarry Drilling and Blasting Cost Structure — The six components of a blasting budget and how to read a contractor quotation.
- Spare Parts Planning and Drilling Downtime — Building a parts package sized to project duration and site remoteness.
Conclusion
A turnkey quarry package is a boundary agreement before it is an equipment list. The rig, the compressor, the tooling, the parts, and the commissioning either sit inside that boundary or they become the buyer's problem at the worst possible moment — which is usually the week the bench is supposed to start producing.
Scope it from the production target backwards. Define the equipment list yourself and make suppliers price against it. Then measure the first month against metres per shift, utilisation, deviation, bit life, and secondary breaking, while the specification is still something you can argue about.
The West African operator saved 22 percent on paper and lost eleven days on the bench. The quotation was accurate. The boundary was just narrower than the word on the cover page suggested.
One question worth putting to your current setup: if you measured hole deviation at the toe on your next blast, what would it cost you in secondary breaking — and would that number change which rig you buy next?
Website: www.welldonemining.com
Email: info@welldonemining.com
Frequently Asked Questions
What should a quarry turnkey drilling package actually include?
At minimum: rig, air supply (onboard or separate compressor), complete tooling package with hammer, bits, rods and adapters at the correct diameter, spare parts sized to project duration, dust suppression, commissioning, operator training, and stated warranty and response terms. Check each line explicitly. The most common omission is the compressor on non-integrated rigs, followed by tooling quantity — one bit and a first fill both appear on a quotation as "DTH bit".
How do I size a rig for my production target?
Work backwards. Tonnage required, divided by rock density, gives blasted volume. Volume divided by burden × spacing × bench height gives hole count. Hole count × depth including subdrill gives drilled metres. Then apply a realistic shift output rather than a raw penetration rate — our quarry drilling solution uses 180–240 metres per 8-hour shift for high-throughput aggregate production, which already includes a utilisation assumption.
DTH or top hammer for a quarry bench?
Depth and hardness decide it. Top hammer drills faster and costs less to run in soft to medium rock (f = 6–14) at depths under 15 metres. Beyond that, energy is lost through the rod string and deviation degrades to ±2–3 percent. DTH handles f = 6–20 across 15–50 metres while holding ±0.5 percent deviation, because percussion is delivered at the bit face. In hard rock or deep benches, DTH is the practical choice.
What benchmarks prove the package was specified correctly?
Metres per shift, rig utilisation percentage, surveyed hole deviation at the toe, bit life in metres, and secondary breaking rate as a share of blasted volume. Start measuring in the first month. Secondary breaking is the one that translates drilling quality into money most directly — deviation below 1.5 percent can reduce it by up to 40 percent, and oversize from misaligned holes can consume 10 to 15 percent of daily output value.
Can Welldone Mining quote a complete quarry package for our site?
Yes. Send your daily production target, rock type and hardness, bench height, target hole diameter and depth, crusher feed size requirement, site elevation, bench width and access gradient, and whether grid power is available at the bench, to info@welldonemining.com. We return a package scoped backwards from that production target, with the air supply resolved inside the quotation and the spare parts coverage stated in operating hours.